Request Quote
Scan the QR code below to connect with us on WhatsApp.
Request Quote
Scan the QR code below to connect with us on WhatsApp.

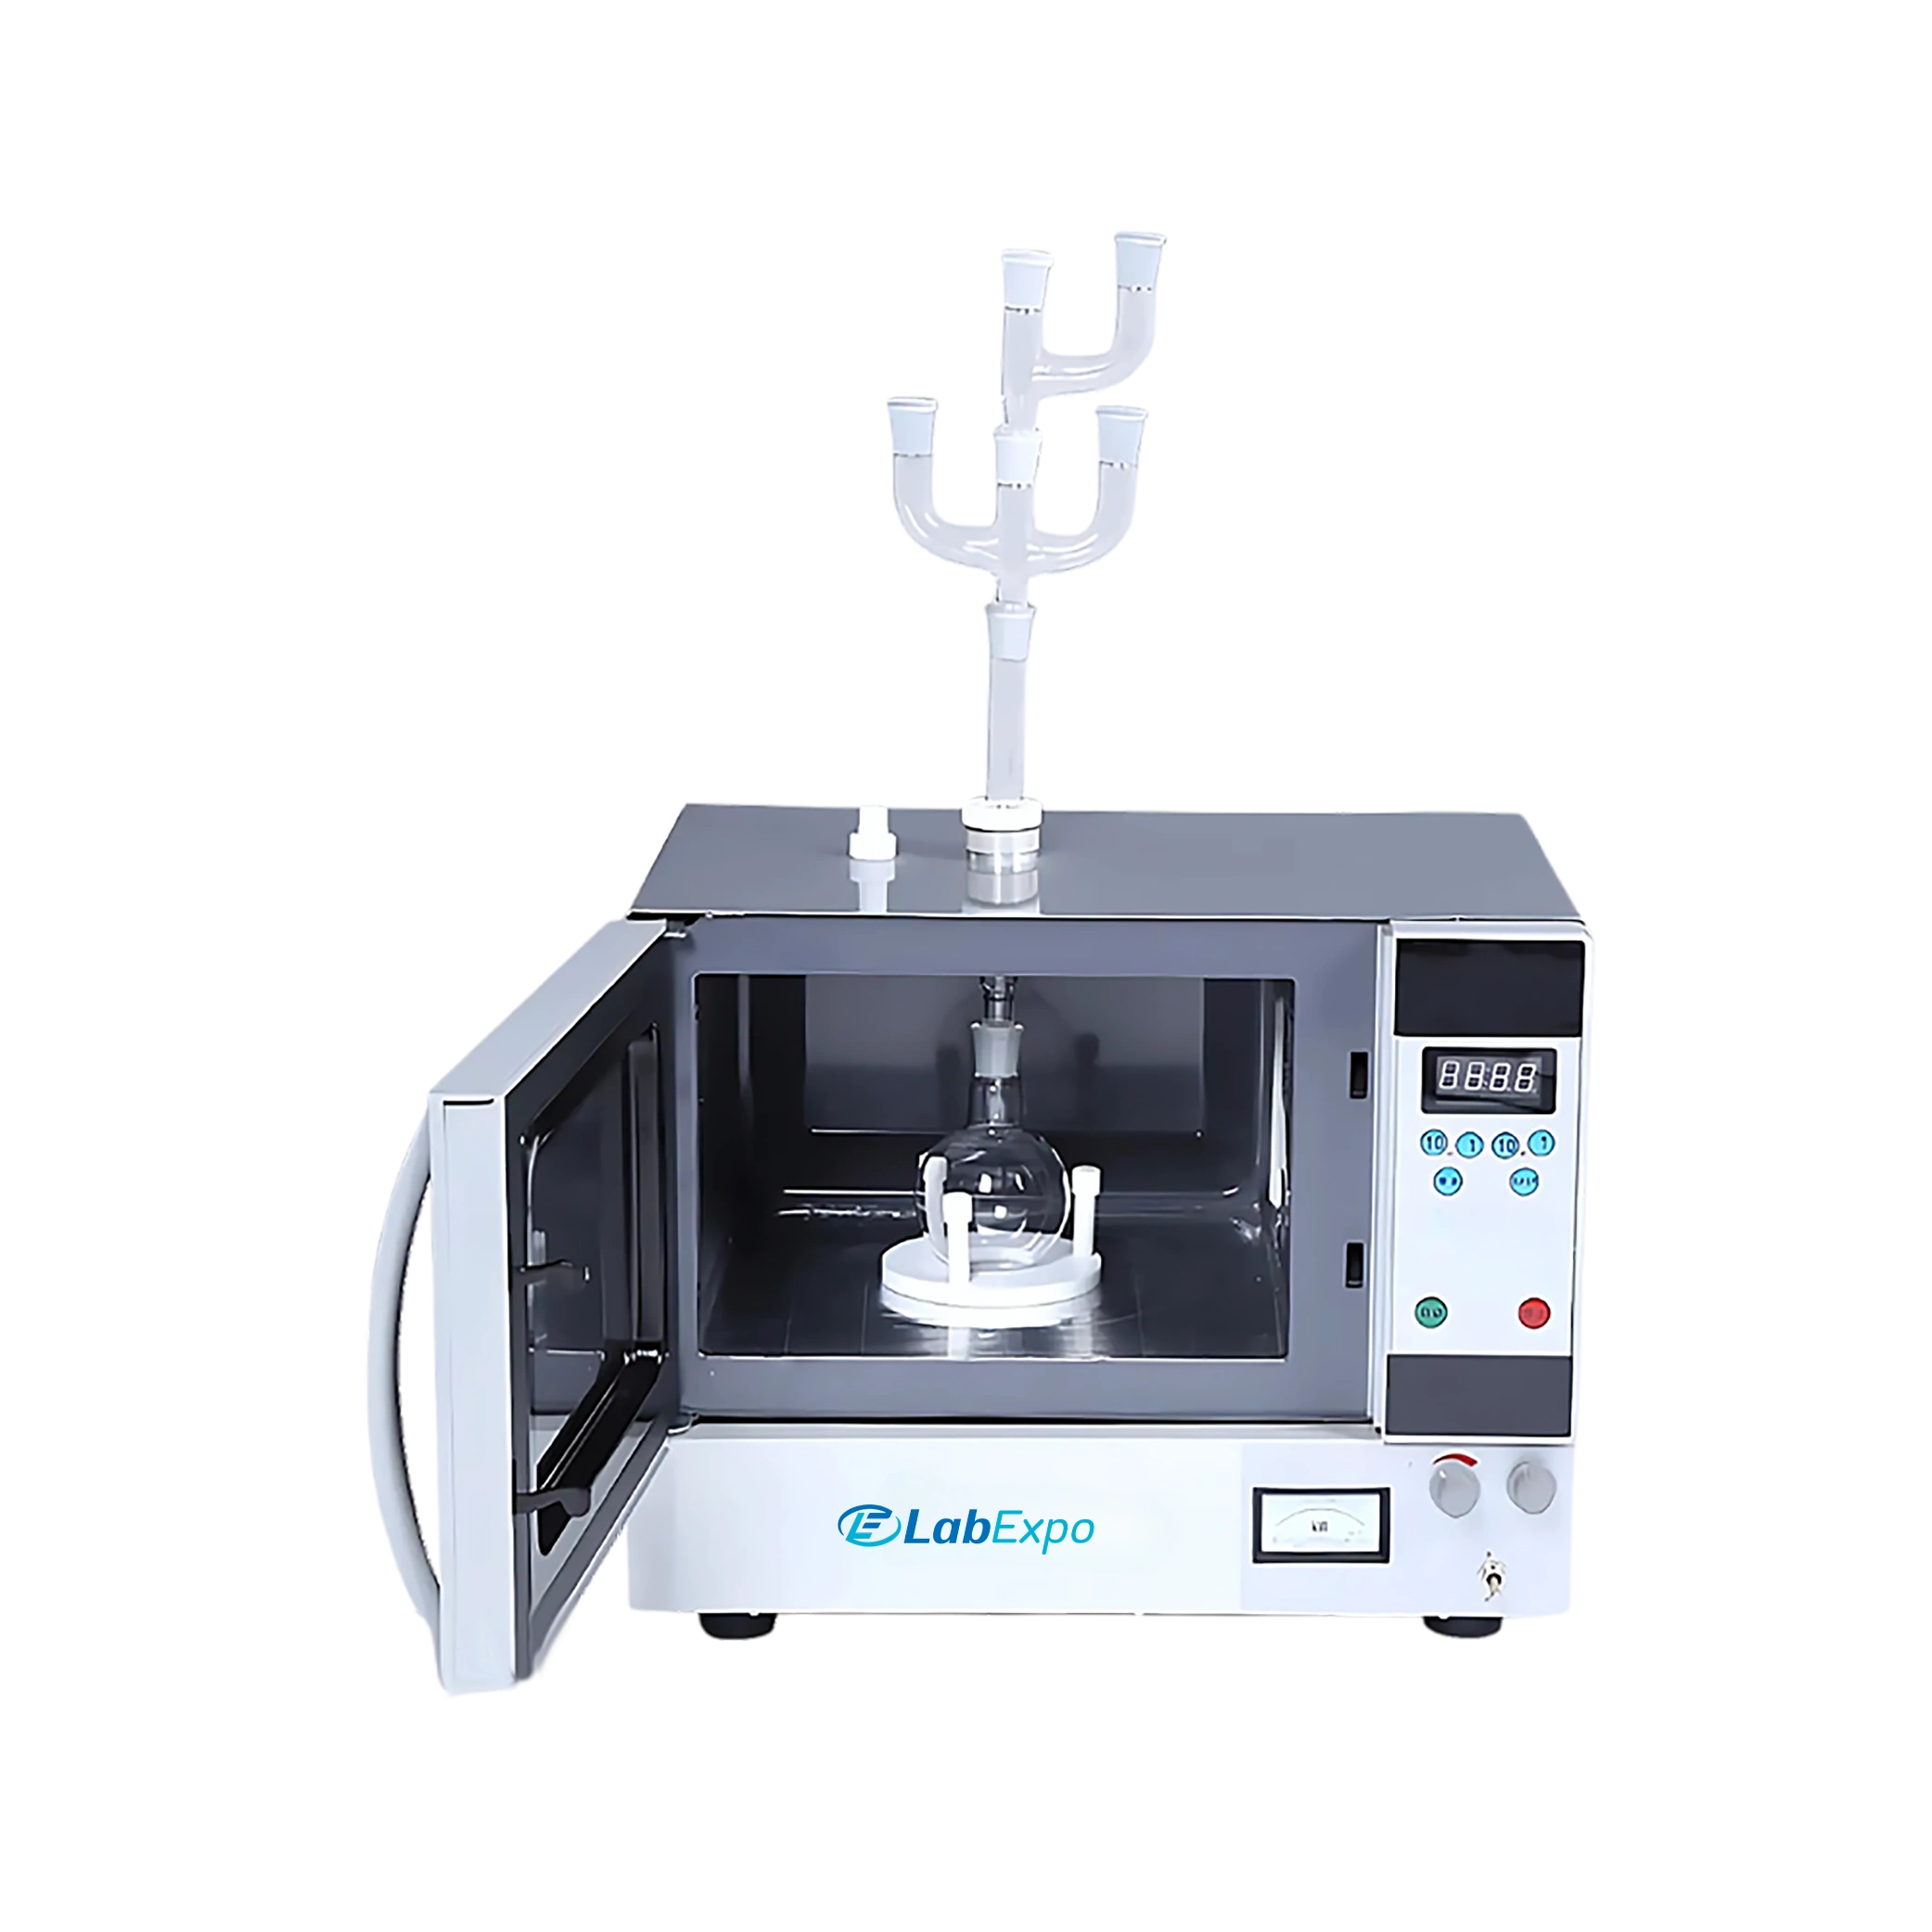


Lab Expo Microwave Chemical Reactor LE-MR102 enables flexible control with finely tunable microwave frequency. It is equipped with an adjustable power setting to accommodate various reaction conditions. Integrated microcomputer control system ensures stable operation and precise regulation. Built-in user-friendly interface simplifies monitoring during experiments. Our Microwave Chemical Reactor is suitable for applications requiring high repeatability in synthesis and catalytic research.
$3,654.00 $ 3045
| Frequency | Adjustable Size |
| Maximum Input Current | 7.8 A |
| Rated Maximum Output Power | 650 W |
| Rated Power Consumption | 1100 W |
| Power Supply | 220 V |
| Chamber Dimension | 290 × 295 × 190 mm |
| Packing Dimension | 610 × 480 × 550 mm |
| Gross Weight | 35 kg |
Function Implementation Chemical synthesis labs 650 W enables controlled microwave-assisted reactions Catalytic research environments Adjustable power setting accommodates various reaction conditions Quality control testing Finely tunable frequency ensures precise reaction regulation Industrial process development Microcomputer control system supports stable operation during experiments Research laboratory workflows User-friendly interface simplifies monitoring of synthesis procedures
Lab Expo Microwave Chemical Reactors are structured around uniform microwave energy coupling to drive controlled reaction acceleration. This microwave reactor integrates precise temperature and pressure regulation with adjustable power output for fine reaction tuning. Real-time monitoring, reinforced pressure containment, and integrated safety interlocks support reproducible synthesis, improved yield control, and efficient operation in chemical, pharmaceutical, and materials research workflows.


